Complex geometry, larger components and awkward access can make familiar checks increasingly difficult. A useful measurement approach starts with the features you need to understand and the decision the result must support.
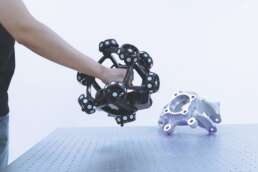
A large fabricated assembly, a curved composite panel or a mould with changing contours can present very different measurement challenges. One may be difficult to move into an inspection area. Another may require information across a surface that individual dimensional checks cannot adequately describe. A third may contain accessible outer geometry alongside recessed features that are harder to capture.
The temptation is to treat all three as a need for more capable equipment. However, “difficult to measure” needs a more precise explanation before an alternative can be assessed. Is the obstacle physical access, the amount of surface information required, the tolerance involved or the effort needed to obtain a usable result?
3D scanning can provide a practical route through some of these challenges. Its usefulness depends on planning the measurement around the component and its purpose, then carrying that plan through to analysis.
Start with the feature or surface that matters
Before deciding how much of a component to scan, establish what needs to be understood. Checking the location of mounting features is a different task from investigating distortion across a panel, even when both concern the same part. The first may require defined dimensional or geometric checks; the second may benefit from broader surface comparison.
Consider a moulded panel that does not sit correctly against its mating structure. Measuring selected mounting points might establish their positions, but leave uncertainty about whether the surrounding surface is contributing to the fit problem. Capturing more of the accessible geometry could help reveal a pattern of bowing or local distortion that warrants further investigation.
That wider coverage is valuable when it answers a relevant question. It also helps determine where detailed capture is needed and where it would add little. Applying the highest resolution everywhere can increase capture and processing effort without improving the result that matters. The measurement plan should therefore identify the features of interest, the required detail and any areas that need a complementary method.
Plan access around the complete measurement task
Large components often make logistics part of the inspection problem. Moving a fabrication, tool or assembly may require lifting equipment, coordination with production and a suitable place to support it. Taking a portable measurement system to the component can reduce some of that disruption, provided the working conditions support the required measurement confidence.
Access still needs careful assessment. Optical scanning requires visibility of the surface being captured; deep recesses, hidden faces and obstructed areas may remain inaccessible. With an optically tracked system, suitable visibility between the tracker and scanner must also be maintained. A workable setup considers the scanning positions, surrounding equipment and any repositioning needed before capture begins.
The support condition matters too. A flexible panel measured loose on a bench may behave differently when located in a fixture or assembly. If the purpose is to understand its installed shape, that distinction could be central to interpreting the result. Temperature, vibration and surface condition should likewise be considered as part of the method.
Planning these details early helps distinguish between a component that can be scanned visually and a measurement task that can be completed reliably.
Establish the reference—and how the part relates to it
A scan records captured geometry. To evaluate that geometry, you need an appropriate reference and a defined comparison method. The reference might be the current CAD model, drawing requirements or a verified reference component, depending on the task. Confirming its revision and suitability avoids investigating differences caused by comparing against the wrong design state.
Alignment determines how the measured part is positioned relative to that reference. This can materially affect the result, particularly on complex surfaces. A best-fit alignment can help explore overall shape differences, but it may distribute deviations in a way that does not represent how the component is located in service.
Returning to the panel example, suppose its mounting features determine its position in the assembly. Referencing the inspection to those features may reveal how the surrounding surface sits once the panel is located. A general best-fit comparison could present a different picture because it positions the geometry to minimise overall differences.
Neither approach should be selected simply because it produces a cleaner-looking colour map. The alignment needs to answer the engineering question, with the chosen reference features and constraints documented so the comparison can be repeated consistently.
Check capability against the actual tolerances
A large, detailed scan does not establish that every feature has been measured adequately. Broad surfaces, small holes, sharp edges and tight radii present different capture and evaluation requirements. Surface visibility, data quality and the method used to calculate a feature all influence the result.
The required tolerance is therefore an essential part of assessing scanning suitability. A method that provides useful evidence of overall distortion may not be appropriate for signing off a small, tightly toleranced feature. The uncertainty associated with the complete measurement process must be considered against the requirement, under the conditions in which the work will actually take place.
For some components, the practical answer is a combination of methods. Scanning can provide wider surface information while probing or CMM measurement addresses selected features. Defining that split around the inspection requirement allows each method to contribute where it is suitable.
This assessment is most meaningful on a representative part. It should examine the features and working conditions that make the application difficult, rather than relying solely on an equipment specification or an uncomplicated demonstration.
Turn the scan into an answer someone can use
A CAD comparison can make variation easier to understand, but a colour map needs context. Its reference, alignment, scale and any gaps in coverage affect what the viewer can reasonably conclude. Where an inspection decision is required, the relevant features, tolerances and evaluation rules need to be included.
The output should make the next action clearer. For a fit investigation, that might mean showing where a surface departs from its expected position relative to the mounting features. For tooling, it could mean documenting the location and extent of a deviation before an adjustment is considered. A dimensional report may be needed alongside the surface visualisation to communicate specific checks.
It is equally important to distinguish observation from explanation. A scan may reveal distortion or a recurring deviation, but identifying its cause can require additional evidence about manufacture, handling or assembly.
A useful report brings together the measured findings, their limitations and the information needed for the next decision. That reduces the risk of passing a detailed dataset to another team without resolving the original question.
What should you look for in a TrackScan Sharp S demonstration?
For larger and complex components, a portable scanning system such as TrackScan Sharp S offers a way to explore surface capture around the part. The useful demonstration follows your application from setup through to the relevant analysis, so you can assess the work involved as well as the visible scan.
Ask to see how the difficult areas would be approached, what coverage can be achieved and which features may need another method. The demonstration should explain how the geometry is referenced, how the required checks are evaluated and what the resulting report would tell you. Preparation, repositioning and processing all belong in the assessment of overall effort.
The strongest outcome is a clear understanding of suitability: which parts of your measurement task the workflow could address, what remains to be proven and whether the result would help your team move forward.
Discuss your difficult component measurement
If complex geometry, component size or awkward access is making inspection harder, share a part image, drawing or CAD model with the T3DMC team.
Tell us which features you need to understand, the tolerances involved and what is difficult about the current method. We can help you explore whether TrackScan Sharp S, a complementary measurement approach or a revised workflow would be appropriate for the result you need. Click the box below to speak to our experts today.